Introduction to Conveyor Chain
Conveyor chains are an essential component in various industries, playing a crucial role in the transportation and handling of materials. They are designed to move products, goods, or bulk materials along a defined path, providing a reliable and efficient means of conveyance. Conveyor chains come in different types, such as roller chains, bush chains, and engineered steel chains, each tailored to specific applications and operating conditions. These chains are widely used in industries like manufacturing, food processing, automotive, mining, and logistics. Their durability, strength, and ability to operate under heavy loads make them indispensable for streamlining production processes and ensuring smooth material flow. Conveyor Chain
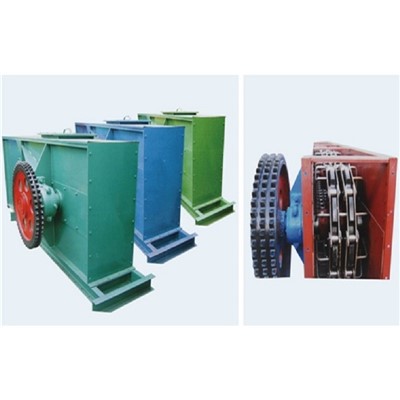
1. Zhejiang Hangte Chain Transmission Co., Ltd.
Zhejiang Hangte Chain Transmission Co., Ltd. is a leading manufacturer of conveyor chains in China. With years of experience in the chain – making industry, the company has established a solid reputation for its high – quality products and excellent service. It is committed to continuous innovation and technological improvement to meet the diverse needs of global customers.
Features in Conveyor Chain
- High – precision manufacturing: The company uses advanced production equipment and strict quality control systems to ensure the dimensional accuracy of conveyor chains. This precision allows for smooth and stable operation, reducing the risk of chain derailment and improving the overall efficiency of the conveyor system.
- Customization capabilities: Zhejiang Hangte Chain Transmission Co., Ltd. can customize conveyor chains according to customers’ specific requirements. Whether it is the chain’s size, material, or special surface treatment, they can provide tailored solutions to fit different industrial applications.
- Wide range of materials: They offer conveyor chains made from various materials, such as carbon steel, stainless steel, and alloy steel. Different materials are selected based on the working environment, such as corrosion – resistant stainless steel for food processing and chemical industries, and high – strength alloy steel for heavy – duty mining applications.
Company Advantages
- Competitive pricing: By optimizing the production process and supply chain management, the company can offer high – quality conveyor chains at a competitive price. This makes their products attractive to both large – scale enterprises and small – and medium – sized businesses.
- Reliable after – sales service: The company has a professional after – sales service team that can provide timely technical support and maintenance services. They are committed to solving customers’ problems quickly and ensuring the long – term stable operation of the conveyor chains.
- Strong R & D strength: With a dedicated R & D team, Zhejiang Hangte Chain Transmission Co., Ltd. can keep up with the latest industry trends and develop new products. They invest a lot in research and development to improve the performance and quality of their conveyor chains.
Website: https://www.chinahtchain.com/
2. Tsubaki Group
Tsubaki Group is a well – known Japanese company with a long – standing history in the power transmission and conveyor chain industry. It was founded in 1917 and has since grown into a global enterprise with a wide range of products and services.
Features in Conveyor Chain
- Advanced heat – treatment technology: Tsubaki uses unique heat – treatment methods for its conveyor chains, which greatly enhances the chain’s hardness, wear resistance, and fatigue strength. This allows the chains to operate for a long time under harsh conditions without significant performance degradation.
- Innovative design: The company is constantly innovating in the design of conveyor chains. For example, they have developed chains with self – lubricating features, which reduce the need for frequent lubrication and maintenance, thereby improving the efficiency and reliability of the conveyor system.
- High – quality materials: Tsubaki selects premium materials for its conveyor chains, ensuring high – level performance. Their materials are carefully tested to ensure they meet strict quality standards.
Company Advantages
- Global presence: Tsubaki has a large – scale global distribution network, which allows it to quickly respond to customer needs around the world. They can provide local service and support, ensuring the timely supply of replacement parts.
- Rich industry experience: With over a century of experience in the industry, Tsubaki has in – depth knowledge of different industrial applications. This enables them to offer the most suitable conveyor chain solutions for various industries, including automotive, food, and electronics.
- Commitment to environmental protection: Tsubaki is committed to developing environmentally friendly products. Their conveyor chains are designed to reduce energy consumption and minimize the impact on the environment during the production and use processes.
3. Rexnord Corporation
Rexnord Corporation is an American company that is a major player in the industrial products market, including conveyor chains. It has a long – standing reputation for providing high – performance and reliable solutions.
Features in Conveyor Chain
- Heavy – duty construction: Rexnord’s conveyor chains are designed for heavy – duty applications. They can withstand high loads, extreme temperatures, and harsh operating environments. For example, in the mining industry, their chains can handle the weight of large amounts of ore and operate in dusty and abrasive conditions.
- Modular design: The company offers a modular design for its conveyor chains, which allows for easy installation, replacement, and expansion. This modular approach reduces downtime during maintenance and upgrades, improving the overall productivity of the conveyor system.
- Integrated solutions: Rexnord provides integrated conveyor chain solutions, which include not only the chains themselves but also related components such as sprockets, bearings, and lubrication systems. This one – stop – shop approach simplifies the procurement process for customers.
Company Advantages
- Engineering expertise: Rexnord has a team of experienced engineers who can provide customized engineering solutions for customers. They can analyze the specific requirements of each application and design the most appropriate conveyor chain system.
- Quality control: The company has strict quality control procedures in place throughout the production process. From raw material inspection to final product testing, every step is carefully monitored to ensure the highest quality of the conveyor chains.
- Wide product portfolio: Rexnord offers a wide range of conveyor chain products, catering to different industries and application needs. Whether it is a light – duty conveyor in a packaging line or a heavy – duty conveyor in a steel mill, they have a suitable solution.
4. Iwis Antriebssysteme GmbH & Co. KG
Iwis is a German family – owned company with a strong focus on precision engineering and high – quality power transmission products, including conveyor chains.
Features in Conveyor Chain
- Precision manufacturing: Iwis is known for its precise manufacturing processes. Their conveyor chains have tight tolerances, which ensure smooth and accurate operation. This precision is especially important in applications where high – speed and high – precision material handling are required, such as in electronics manufacturing.
- Silent operation: The company has developed conveyor chains with low – noise features. These chains use special designs and materials to reduce the noise generated during operation, creating a more comfortable working environment.
- Flexible chain designs: Iwis offers a variety of flexible conveyor chain designs, which can be easily adapted to different conveyor layouts. They can be bent, curved, or twisted to fit complex installation requirements.
Company Advantages
- Long – term innovation tradition: Iwis has a long – standing tradition of innovation. They continuously invest in research and development to introduce new technologies and improve the performance of their conveyor chains.
- Customer – oriented approach: The company focuses on providing excellent customer service. They work closely with customers to understand their needs and provide customized solutions. Their technical support team is always available to assist customers.
- Sustainable production: Iwis is committed to sustainable production. They use eco – friendly materials and processes in the production of their conveyor chains, and also focus on energy efficiency during the manufacturing process.
5. Renold plc
Renold is a British company with a history dating back to 1879. It has a strong reputation in the chain manufacturing industry and is well – known for its high – quality conveyor chains.
Features in Conveyor Chain
- High – strength chains: Renold’s conveyor chains are engineered to provide high strength and durability. They can withstand high – impact loads and heavy – duty applications, making them suitable for industries such as automotive manufacturing and heavy machinery.
- Corrosion – resistant coatings: The company offers conveyor chains with corrosion – resistant coatings, which protect the chains from rust and corrosion in harsh environments. This is particularly important in industries such as food processing and marine applications.
- Specialty chains: Renold manufactures specialty conveyor chains for specific applications, such as chains with special attachments for handling irregularly shaped objects or chains for high – temperature applications.
Company Advantages
- Historical brand value: Renold’s long – standing history has established a strong brand image. Customers trust the quality and reliability of their products, which gives the company a competitive edge in the market.
- Global service network: Renold has a global service network that can provide quick and efficient support to customers around the world. They can supply replacement parts and offer on – site maintenance services.
- Industry – leading technology: The company invests in advanced manufacturing technologies to improve the quality and performance of its conveyor chains. They are constantly researching and developing new products to meet the evolving needs of the market.
6. Diamond Chain Company
Diamond Chain Company is an American firm with a long – established presence in the chain manufacturing industry. It has a deep understanding of the requirements for different conveyor chain applications.
Features in Conveyor Chain
- Enhanced wear resistance: Diamond Chain uses advanced manufacturing techniques and materials to enhance the wear resistance of its conveyor chains. This allows the chains to have a longer service life, reducing the frequency of chain replacements and maintenance costs.
- Standardized products: The company offers a wide range of standardized conveyor chain products, which ensures easy availability and compatibility. Standardization also simplifies the procurement process for customers, as they can easily find the right chain for their conveyor systems.
- Specialized chain series: Diamond Chain has developed specialized conveyor chain series for different industries, such as food – grade chains for the food industry and heavy – lift chains for the construction industry.
Company Advantages
- Product consistency: Diamond Chain is known for the consistency of its product quality. Customers can expect the same high – level performance from every batch of conveyor chains they purchase, which is crucial for maintaining the stability of the conveyor system.
- Technical support: The company provides comprehensive technical support to its customers. Their technical experts can offer advice on chain selection, installation, and maintenance, helping customers optimize the performance of their conveyor systems.
- Cost – effectiveness: By optimizing the production process and supply chain, Diamond Chain can offer cost – effective conveyor chain solutions without sacrificing quality. This makes their products a popular choice among cost – conscious customers.
7. Wippermann Ketten GmbH & Co. KG
Wippermann is a German company that specializes in the production of high – quality chains, including conveyor chains. It has a reputation for precision engineering and reliable products.
Features in Conveyor Chain
- High – precision pitching: Wippermann’s conveyor chains feature high – precision pitching, which ensures smooth and accurate movement on the conveyor. This precision is essential for applications where precise material positioning is required, such as in the pharmaceutical and electronics industries.
- Hygienic design: For applications in the food and beverage industry, Wippermann offers conveyor chains with a hygienic design. These chains are easy to clean and prevent the accumulation of dirt and bacteria, ensuring compliance with strict food safety regulations.
- High – performance materials: The company uses high – performance materials in its conveyor chains, which can withstand high – speed operation and heavy loads. Their materials are carefully selected and treated to ensure optimal performance.
Company Advantages
- German engineering quality: As a German company, Wippermann adheres to strict German engineering standards. This ensures that its conveyor chains are of the highest quality and reliability, giving customers confidence in their products.
- Continuous improvement: Wippermann is committed to continuous improvement. They regularly update their production processes and product designs to meet the changing needs of the market and improve the performance of their conveyor chains.
- Custom – made solutions: The company can provide custom – made conveyor chain solutions according to customers’ specific requirements. Their engineering team can design and manufacture chains with unique features to fit special applications.
8. Jasper Engines & Transmissions (Chain Division)
Jasper is an American company well – known for its remanufactured engines and transmissions. Its chain division also produces high – quality conveyor chains.
Features in Conveyor Chain
- Complementary product approach: Since Jasper is involved in engine and transmission manufacturing, its conveyor chains are often designed to be complementary to the entire production process. This means that the chains can work well with other equipment in the production line, improving the overall efficiency of the manufacturing process.
- Reconditioned chain options: In addition to new conveyor chains, Jasper offers reconditioned chains. These reconditioned chains are thoroughly inspected, repaired, and tested to ensure they meet the same performance standards as new chains. This provides a cost – effective alternative for customers.
- Close – fit to equipment: The conveyor chains produced by Jasper are designed to have a close fit with the sprockets and other components of the conveyor system. This reduces wear and tear and improves the overall reliability of the conveyor.
Company Advantages
- Integration with overall production: The ability to integrate conveyor chain production with the larger engine and transmission manufacturing business gives Jasper an advantage in understanding the overall production requirements. They can provide holistic solutions to customers.
- Quality reconditioning process: The reconditioning process of Jasper’s conveyor chains is highly standardized. Every reconditioned chain goes through a rigorous testing process to ensure its quality, providing customers with a reliable and cost – effective option.
- After – market support: Jasper has a strong after – market support system. They can supply replacement parts for their conveyor chains and offer technical support to customers who use their chains, ensuring the long – term operation of the conveyor systems.
9. Doubly – Link Chain Co., Ltd.
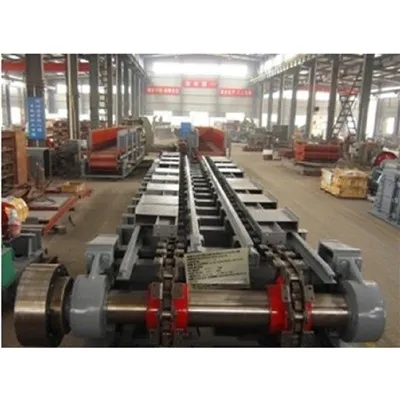
Doubly – Link Chain is focused on providing high – quality chain products, including conveyor chains, and has a certain influence in the market.
Features in Conveyor Chain
- Good lateral flexibility: The conveyor chains of Doubly – Link Chain have good lateral flexibility, which allows them to be easily adapted to curved conveyor systems. This flexibility expands the application scope of the chains in various industrial scenarios.
- Efficient material transfer: The design of their conveyor chains is optimized for efficient material transfer. They can move materials smoothly and quickly, reducing the transfer time and improving the productivity of the conveyor system.
- Cost – effective solutions: The company offers cost – effective conveyor chain solutions. By using efficient production processes and cost – control measures, they can provide high – quality chains at a reasonable price.
Company Advantages
- Quick response to orders: Doubly – Link Chain has a fast – paced production and order – fulfillment system. They can quickly respond to customers’ orders and ensure timely delivery, which is important for customers who need to keep their production lines running continuously.
- Flexible production capacity: The company has a flexible production capacity, which can adjust the production volume according to customers’ needs. Whether it is a small – batch order or a large – scale production requirement, they can meet the demand.
- Technical innovation: Doubly – Link Chain is committed to technical innovation. They invest in research and development to improve the performance of their conveyor chains and introduce new features to meet the changing market needs.
10. TIDLAND MEGADYNE S.p.A.
Bucket Elevator Chain TIDLAND MEGADYNE is an Italian company that offers a wide range of industrial products, including conveyor chains.
Features in Conveyor Chain
- High – speed operation suitability: Their conveyor chains are designed to be suitable for high – speed operation. They can maintain stable performance at high speeds, reducing the risk of chain breakage and improving the efficiency of fast – paced production lines, such as in the packaging industry.
- Resistance to chemical substances: For applications in industries where exposure to chemicals is common, TIDLAND MEGADYNE’s conveyor chains are resistant to various chemical substances. This property extends the service life of the chains in harsh chemical environments.
- Ergonomic design: The company pays attention to the ergonomic design of its conveyor chains. Chains are easy to install and maintain, reducing the workload on operators and minimizing the time required for maintenance.
Company Advantages
- Italian design and craftsmanship: TIDLAND MEGADYNE combines Italian design aesthetics with high – quality craftsmanship. Their conveyor chains not only perform well but also have an attractive appearance.
- Global sales and service: The company has a global sales and service network. They can provide customers around the world with professional product information, technical support, and after – sales service, ensuring a seamless customer experience.
- Product diversification: In addition to conveyor chains, TIDLAND MEGADYNE offers a variety of related industrial products. This diversification allows them to provide comprehensive solutions to customers, meeting multiple needs in one place.
